Method for Checking the Gear Strength of Weaving Machine Reducer under Frequent Forward and Reverse Operating Conditions
1、 Structural optimization: improving torque density from the perspective of transmission principle
Adopting a multi tooth synchronous meshing structure, such as a cycloidal reducer or a planetary reducer with a high number of planetary gears, by increasing the number of teeth meshing simultaneously (from 50% to 60%~70%), the load is shared by more tooth surfaces, and greater torque is output under the same volume.
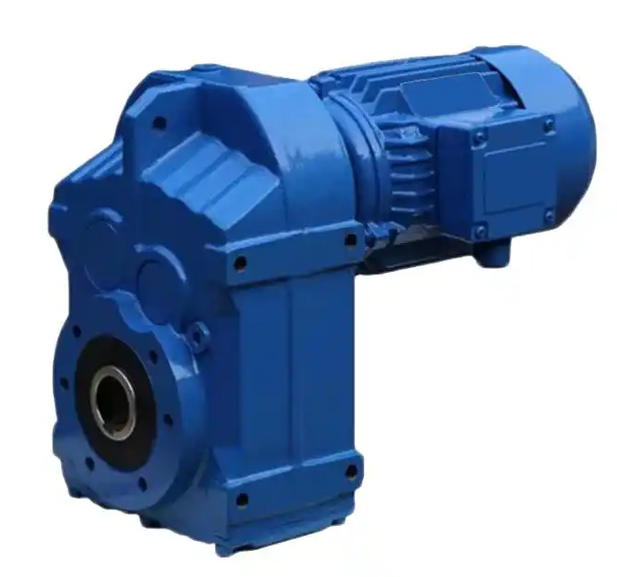
Optimizing gear parameters: increasing the gear module, adopting helical gears or angle modified gear designs, increasing tooth width and contact area, can improve load-bearing capacity by 20% to 30%; Adjusting the displacement coefficient and adopting a 25 ° pressure angle design can also improve the strength of the tooth root.
Adopting a hollow output shaft design: allowing cables and pipelines to pass through the axis, transmitting power and reusing space, reducing peripheral occupation, and compressing the overall installation space by more than 25%.
2、 Material and process strengthening: Enhancing load-bearing capacity without increasing size
Core component material upgrade: The gears are made of high-strength carburizing and quenching alloy steel (such as 20CrMnTi, 17CrNiMo6), with a tooth surface hardness of HRC58~62 and a core that maintains toughness; Upgrade the bearing to a double row tapered roller bearing, achieving torque upgrade under the same housing size.
Surface strengthening treatment: Ion nitriding on the tooth surface (hardness ≥ 60HRC), PVD coating on the needle tooth sleeve (friction coefficient reduced to 0.03), to enhance anti bonding and wear resistance.
Precision machining and assembly: using five axis CNC forming grinding to control tooth profile error of 3-5 μ m; Accurately pre tighten the bearings to eliminate clearance, improve radial and axial rigidity, and ensure even load distribution.
3、 Specific directions for customized renovation
Precise speed ratio matching: Customize non-standard speed ratios based on the actual speed requirements of the air-jet loom, and amplify torque through a reasonable reduction ratio while meeting the beat (output torque=motor torque x reduction ratio x efficiency).
Customization of flanges and installation methods: For compact layout of weaving machines, special flange interfaces or foot type installation can be customized to achieve direct connection without modification and reduce installation redundancy space.
Lubrication and heat dissipation upgrade: Due to poor heat dissipation conditions in compact spaces, high-pressure oil injection lubrication (oil pressure ≥ 0.25MPa) or circulating oil cooling systems are required; Casting micro heat dissipation fins on the surface of the shell increases the heat dissipation area by 30% to 40%, preventing lubrication failure caused by high temperature.
Improvement of input connection structure: Adopting a detachable connection with a U-shaped shaft and U-shaped hole instead of a flat key connection, shortening the length of the input end, making the fit closer to the bearing, and improving the stability of torque transmission.