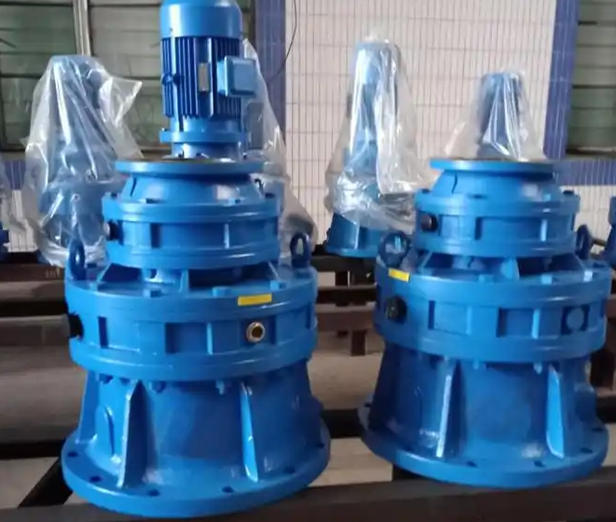
What are the methods for straightening the bent output shaft of the BLED141-289 cycloidal reducer
1、 Straightening methods adapted to different bending amounts
1. Twisting straight axis method
Suitable for slight bending scenarios with a bending amount of less than 0.1mm. Fix the shaft on the V-shaped frame and use a copper hammer to evenly twist along the concave surface of the shaft in the circumferential direction, gradually restoring the straightness of the metal fiber extension. The process is simple and the stability is good after straightening.
2. Direct axis method of press machine
Suitable for moderate bending with a bending amount of 0.1~0.5mm. Support the two ends of the output shaft with V-shaped blocks, bend the convex surface upwards, and slowly apply pressure to the convex vertex through a press machine. After overpressure of 0.03-0.05mm, hold the pressure for 5-10 minutes. After unloading, retest the straightness.
3. Local hotspot straightening method
Suitable for shaft segments with localized concentrated bending. Use an oxygen acetylene flame to quickly heat the curved convex surface of the shaft to 600-700 ℃ (dark cherry red), then quickly cool it with compressed air or water mist, relying on the contraction effect of thermal expansion and contraction to complete straightening. Experienced operators are required to operate it to avoid hardening and cracking of the shaft surface.
4. Internal stress relaxation method
Suitable for heavy-duty output shafts with large diameters and large bending amounts. Heat the entire shaft to a temperature range below the quenching and tempering temperature (about 300-400 ℃), while applying constant pressure on the curved convex surface. Utilize the characteristic of internal stress relaxation of the material at high temperatures to gradually correct the bending, and maintain excellent accuracy after straightening.
2、 Key supporting requirements for school administration
Before straightening, a dial gauge must be used to accurately measure the full axis bending distribution on the V-shaped frame, mark the position of the maximum bending point, and control the final straightness of the output shaft of the cycloidal reducer within ≤ 0.02mm/m.
After all straightening is completed, a low-temperature stress relief tempering treatment at around 200 ℃ must be carried out to eliminate the internal stress generated by straightening and avoid rebound and bending during subsequent operation.
If the bending amount of the shaft exceeds 0.5mm or surface cracks or fatigue damage appear after straightening, it is not recommended to continue straightening. It is safer to directly replace the 45 # steel quenched and tempered new output shaft.